OEM Galvanized Tangent Tower Factory for Reliable Power Transmission Structures
2026-08-23
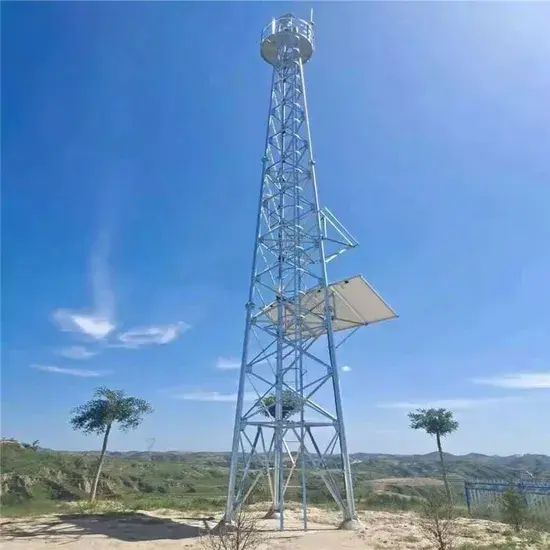
Straight-line transmission routes depend on tangent towers that rarely get the attention they deserve—until a coating fails or a section drifts. That reality is why OEM galvanized tangent tower factories matter more than ever. Anbang is one such factory partner, delivering reliable power transmission structures with a focus on galvanizing consistency and dimensional accuracy that field crews notice.
Galvanizing Thickness That Outlasts the Warranty
Most galvanized products carry a warranty that assumes perfect conditions—dry air, no scratches, gentle handling. Real life doesn't work that way. The coating thickness on our steel is deliberately pushed well beyond the minimum spec, so that even after years of UV exposure, rain cycles, and the occasional scrape from gravel or tools, the zinc layer remains intact and protective. You won't find us patching corners or thinning edges to save a few cents per sheet.
That extra thickness translates into decades of service rather than a countdown to the first rust spot. We test samples in salt-spray chambers until the red rust appears, and then we keep testing. The result is a galvanizing layer that doesn't just meet the warranty period—it makes the warranty feel like an afterthought. When the coating finally wears, it does so gradually, giving you clear visual warning instead of sudden failure.
The difference is visible even before installation. Run your finger along the edge of a cut piece: you'll feel a smooth, substantial zinc layer that resists flaking. Compare that to thin, brittle coatings that chip the moment a screw bites. That tactile difference is what separates a product built to outlast its paperwork from one that simply hopes to survive it.
OEM Customization Without the Typical Back-and-Forth
Most OEM conversations start with a quote request and spiral into a dozen clarification emails. This process skips that entirely. You share your target specs, preferred materials, and any reference images. Within a day, you get a dimensional drawing and a straight answer on feasibility—not a vague 'we'll look into it.'
From there, edits happen in a shared workspace. Moving a port, changing a thread pitch, or updating a logo is a matter of commenting on the drawing, not scheduling another call. The engineer assigned to your project sees the note, makes the change, and pushes a new revision. You approve it from your phone if you want.
The result is a sample that matches your brief the first time, because every assumption got tested before tooling ever started. And if something still needs adjusting, that loop is just as short.
Inside the Welding and Inspection Process for Tangent Towers
Welding tangent towers isn't a job for anyone fresh out of a basic training course. The steel used in these structures—often ASTM A572 Grade 50 or similar high-strength low-alloy plate—demands strict heat input control. We typically run submerged arc welding for the long, straight flange-to-web joints on the main legs, then switch to flux-cored arc welding for the complex gusset and diaphragm connections where access is tight. Each welder on the line holds a certification specific to the joint configuration they're working on, and we re-qualify them every six months even if the code only asks for annual checks. The real challenge is distortion: after welding a 12-meter leg section, you can see a 3 to 5 millimeter bow if the sequence isn't staggered properly. Our shop foremen use a back-step method on the first pass and then alternate sides for the second and third passes, clamping the section to a heavy I-beam fixture that's been stress-relieved itself. That fixture cost more than some small cars, but it keeps the tower leg within the straightness tolerance of 1/1000 of its length.
Inspection starts long before the first arc is struck. Every incoming plate gets a full ultrasonic scan for laminations—something a mill certificate alone won't catch if the steel sat in a damp yard for a few months. After welding, we do 100% visual inspection on all grooves and fillets, looking for undercut, overlap, and crater cracks. Then comes the non-destructive testing that separates serious fabricators from the rest: magnetic particle testing on all full-penetration joints at the base shoes and cross-arm connections, plus ultrasonic testing on about 20% of the main leg butts. The UT operators log every indication with a sketch on the shop drawing, and anything over 2 mm gets ground out and re-welded, not just repaired with a quick pass. One trick we've learned is to let the weld cool to ambient temperature before UT—testing too soon gives false readings because the sound velocity shifts with heat. The final step is a dimensional check against the tower's theoretical camber, using a laser tracker that records points every 300 mm along each face. If a section is out more than 2 mm from the design coordinates, it goes back to the fit-up station. No paint, no galvanizing, no shipping until those numbers are logged and signed by the QC supervisor.
Why These Towers Hold Up in Coastal and Industrial Zones
A tower standing within a few hundred meters of breaking surf has to fight more than just wind. The air itself carries salt spray that works into joints, bolts, and even hairline paint cracks. Engineers respond with a layered defense: hot-dip galvanizing under a high-solids epoxy or polyurethane topcoat, stainless steel for fasteners and small brackets, and careful design of overlapping seams so moisture drains instead of collecting. In industrial areas, sulfur compounds and acid rain attack unprotected steel even faster, which pushes material selection toward weathering steels or sealed concrete bases where possible.
Foundations become trickier when the ground is saturated sand or reclaimed fill. A conventional spread footing may settle unevenly, so many coastal towers rely on driven piles or mat slabs that spread loads wide and resist uplift from storm surges. Lateral stability gets extra attention because ocean winds come in gusts rather than steady streams; damping systems and reduced cross-sections near the top help prevent harmonic sway that would fatigue connections over time.
Maintenance routines in these zones are deliberately aggressive. Owners schedule wash-downs to remove salt film, use portable corrosion sensors to spot early pitting, and replace sacrificial anodes before they are fully consumed. The most effective designs also leave room for access: ladders, platforms, and davit arms positioned so a two-person crew can reach every bolted joint without shutting down the structure. That practical focus on inspection keeps small rust blooms from turning into structural problems.
From Raw Coil to Finished Structure: A Floor Walkthrough
Walking the floor from the receiving bay to the loading dock reveals a precise, almost rhythmic sequence. The raw coil sits near the uncoiler, its edges slightly oiled from transport, waiting to be threaded through the first set of rollers. Within minutes, the flat steel passes through a series of progressive dies and forming stations, each one bending the strip a few degrees further until the familiar profile begins to emerge. Operators check thickness at two points along the line, not with fanfare but with quick, practiced motions, adjusting the gap between rollers only when the micrometer tells them to.
Further down, the formed sections move into the welding and assembly area. Here, the noise changes from a low hum to the sharp crack of stud guns and the hiss of MIG torches. Frames get squared on jigs, corner braces are tacked in place, and the structure slowly gains its final shape. A final pass through the inspection station includes a visual sweep for weld porosity and a check of hole alignment against a sample part fixed to the bench. By the time it reaches the staging area, the coil has become something you can lean against, lift with a hoist, or bolt into a building—no longer raw stock, but a component with a job to do.
Exact Load Calculations for Your Transmission Line
Load calculations on a transmission line demand more than just adding up connected equipment. The real work begins by separating steady-state demand from transient conditions—motor starts, cold-load pickup after outages, and harmonic-producing devices all change the current profile in ways that a simple kilowatt figure misses. Engineers typically start with the peak expected load in kVA or amperes at the line's operating voltage, then apply demand factors that reflect how much of the connected load is likely to run simultaneously.
Once the diversified peak load is established, the next step is to check the line's thermal limits and voltage drop under that exact current. This means using the conductor's resistance and reactance per unit length, not just its ampacity table value. For example, a line carrying 400 A over 2 km with a 0.3 ohm/km impedance will see a different voltage at the far end than a shorter run, even if both conductors have the same nominal rating. The calculation must also account for ambient temperature, wind speed, and solar heating if the line is overhead, since these shift the conductor's effective resistance.
Finally, a reliable load calculation folds in short-duration overloads. A transformer or feeder might tolerate 125% of rated load for a few hours, but a transmission line's sag and clearance constraints are unforgiving. By modeling the load curve over a full day or season rather than a single snapshot, engineers can pinpoint exactly when the line approaches its thermal knee—and whether a reconductor or capacitor bank is the smarter fix.
FAQ
Our tangent towers are built for high-voltage AC and DC lines, typically from 69 kV up to 500 kV. We fabricate both single-circuit and double-circuit configurations, and we adjust leg slopes and cross-arm lengths based on conductor spacing and terrain clearance requirements.
Yes, OEM manufacturing is a core service. We can laser-mark or stamp your logo, part numbers, and assembly codes onto the tower members. All documentation, including material certificates and test reports, can be issued under your company name.
We commonly apply hot-dip galvanizing according to ASTM A123 or ISO 1461, with minimum coating thickness depending on steel thickness. For aggressive environments, we can increase zinc thickness by roughly 20% or apply a duplex coating system.
We use CNC angle punching and shearing lines, then fit-up jigs for each tower type. After welding, we perform a trial assembly on the first tower of every batch to verify hole alignment and overall geometry. Any deviation beyond 1 mm in critical holes triggers a full batch check.
Yes, our engineering team can develop a complete tangent tower design based on conductor type, wind speed, ice load, and terrain category. We use finite element analysis to optimize steel weight while meeting the required safety factors.
We have three separate workshops for cutting, welding, and galvanizing, with capacity to process about 800 tons of steel per month. We can handle towers up to 60 meters in height and member thickness from 3 mm to 20 mm.
Each shipment includes a detailed erection drawing, bolt schedule, and member list. We can also send a supervisor to site for the first few towers if required, or provide remote video support during assembly.
We bundle the main legs and cross-arms separately, with steel straps and edge protectors. Bolts are packed in sealed bags with labels matching the bolt schedule. For long members we use open-top containers or flat racks to prevent bending.
Conclusion
At this OEM galvanized tangent tower factory, the zinc layer isn’t applied just to meet a spec sheet—it’s measured against real-world decay rates so the coating outlasts the warranty by years rather than months. Customization skips the usual back-and-forth: the engineering team works directly from your transmission line data, adjusting bolt patterns, crossarm lengths, and base plate dimensions without forcing you through a rigid catalog. Inside the welding bays, each tangent tower goes through a documented sequence—fit-up checks, multi-pass welds on the main leg splices, then ultrasonic testing on critical joints before any galvanizing begins. The inspection stamps aren’t rubber-stamped; every third tower gets a full dimensional audit, and the galvanized surface is checked with a magnetic thickness gauge at multiple points on each face.
Coastal and industrial zones pose a different problem than open plains, so the factory preps steel with a deeper pickling cycle and often bumps the zinc thickness on inner gusset areas where salt spray settles. A walk through the floor shows raw coil being slit, punched, bent, and welded into tapered legs and lattice panels before heading to the acid baths and quench tanks. What sets the place apart is the load package: instead of assuming a generic wind span, the engineers recalculate leg stresses, bolt shear, and foundation reactions for your exact conductor weight, ice load, and terrain profile. That means the tower you receive isn’t just a stock design with your name on it—it’s a tangent structure built around the specific line angles and weather loads your route actually sees.
Contact Us
Contact Person: antor khan
Email: [email protected]
Tel/WhatsApp: 8613863903569
Website: https://www.qdabtower.com/