Which Video Measuring Machine Brand Should You Choose for Precision Inspection?
2026-10-05
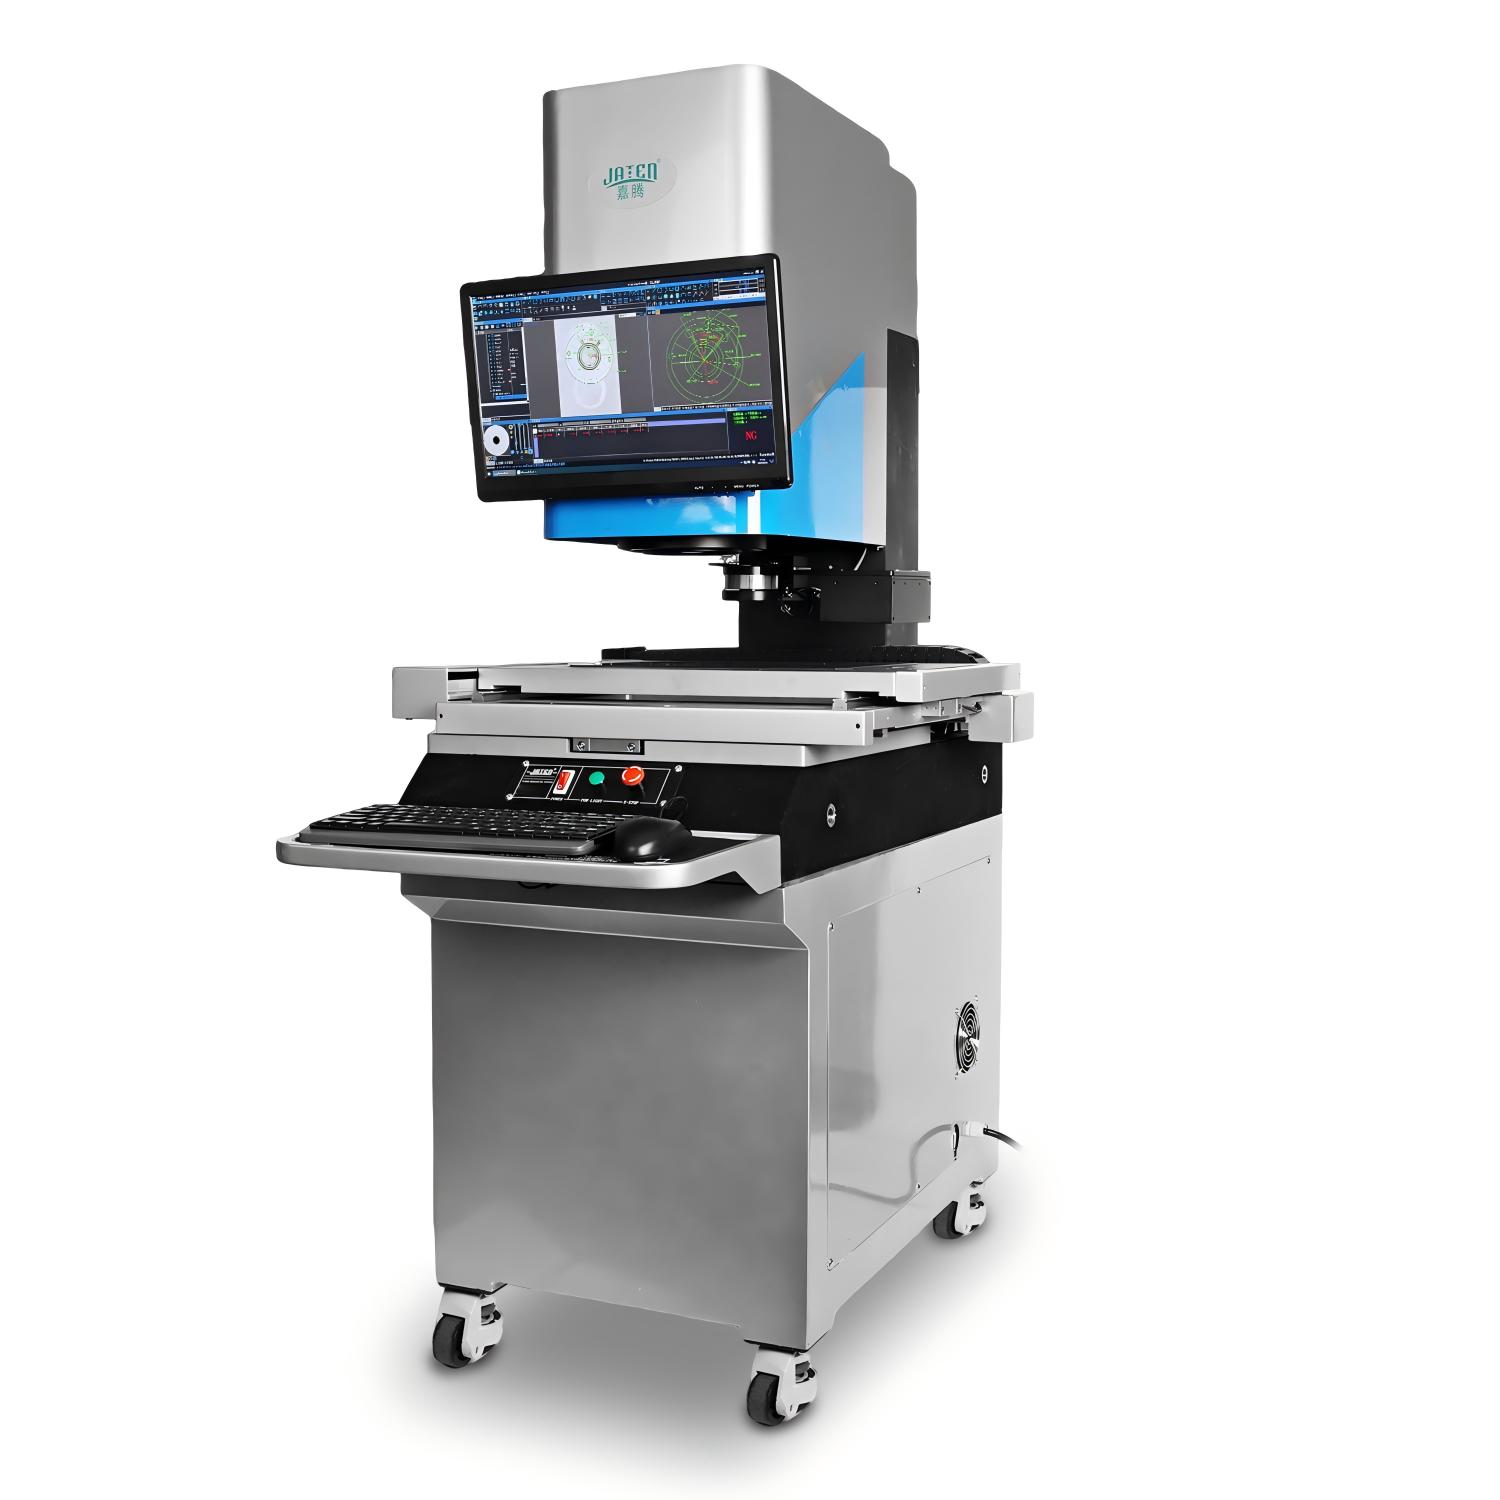
Precision inspection doesn't forgive guesswork. The video measuring machine you pick will either expose hidden defects or let them slip through—and that distinction often comes down to brand. While many names promise micron-level repeatability, few can back it up in real production environments. That's why savvy quality teams are looking closer at JATEN. Before you settle for a spec sheet, let's dig into what actually separates a reliable VMM from the rest.
Why accuracy claims on spec sheets rarely survive first contact with your parts
A tolerance listed as ±0.005 mm assumes the part was measured in a temperature-controlled room, with the probe exactly perpendicular, on a surface that hasn't seen a single chip or burr. Your actual setup probably involves a hand-held caliper, a fixture that flexes under clamping pressure, and a batch of raw stock that wandered through three different heat-treat cycles. The number on the sheet isn't a lie; it's just an answer to a question nobody asked on the shop floor.
Material suppliers love to quote dimensional stability for fully aged, stress-relieved samples. Then you machine a pocket into one side and watch the whole thing bow overnight. Thermal expansion, residual stress, even the order of operations change the geometry before you've taken a second measurement. Spec sheets rarely account for what happens after the first cut, the first torque, or the first time the part sits in a humid bin for a week.
There's also the quiet gap between what the metrology lab reports and what the drawing actually needs. A surface finish Ra of 0.8 μm might be verified on a pristine area, while the sealing face next to a drilled hole is never checked. Once you stack half a dozen 'minor' deviations, the assembly either binds or leaks. That's when the spec sheet gets quietly re-filed and the real numbers come from fit, function, and a bit of careful shimming.
The three brands that dominate precision inspection—and where each falls short
When you look at the installed base in aerospace and automotive metrology rooms, three names appear with almost monotonous regularity: Hexagon, Zeiss, and Renishaw. Together they account for the bulk of CMM sales, probing systems, and software licences. Yet their dominance obscures a simple truth—none of them offers a complete solution without a significant compromise somewhere.
Hexagon’s strength is breadth: its PC-DMIS software and global support network are hard to match. However, the very scope of its portfolio makes upgrades feel like navigating a small enterprise resource planner, and users frequently complain about the learning curve for newer modules. Zeiss, by contrast, excels in optical and tactile precision, but its premium pricing locks out smaller shops, and its proprietary CALYPSO environment can be inflexible when integrating third-party sensors or custom automation.
Renishaw, the de facto standard for touch-trigger probes and machine calibration, suffers from a narrower focus. Its hardware is exceptional, but the lack of a full-fledged CMM software ecosystem forces many customers to pair it with competitor analysis packages, which sometimes leads to compatibility friction. For a quality manager choosing a primary inspection platform, the decision often comes down to which shortfall hurts least.
How to test a video measuring machine before you commit to a purchase
Don't judge a video measuring machine by the demo alone. Bring at least one real part from your production line, preferably with a tight tolerance or a tricky edge, and ask the vendor to measure it while you watch. Then ask them to leave the room and do it again yourself. If the software makes you hunt through menus for basic alignments or the edge detection flips between light and dark on the same feature, that's a red flag. Repeatability matters more than a single flashy reading. Run the same measurement ten times without moving the part; a drift of more than a micron or two usually points to stage slop, thermal drift, or weak edge algorithms.
Bring your own reference standard too. A calibrated ring gauge or a glass scale works fine, but don't stop there. Check the far corners of the measurement envelope, because lens distortion and backlight unevenness rarely show up in the center. Measure a known hole at the middle, then the same size hole near the edge of the field. If the error grows, ask whether the software compensates for that or just hides it. Also pay attention to manual override. On a burr, a chamfer, or a shiny surface, even good auto edge detection will occasionally fail. If a skilled operator can't correct that in two or three clicks without restarting the program, you'll lose time on every inspection.
Finally, test the whole routine you'd actually run on the floor, not the vendor's prepared script. Load a new part, create a simple measurement from scratch, and see how long it takes to get a stable program. While it's measuring, nudge the table lightly or change the room lighting a little. A solid machine should stay within tolerance, not jump by several microns. Ask about calibration intervals and whether software updates are included or a recurring cost. If the answers are vague, walk away.
Optical, laser, or touch probe: which measurement method matches your inspection workflow
Choosing between optical, laser, and touch probe measurement often comes down to what you're actually trying to inspect, not just which technology sounds newest. Touch probes remain the workhorse for dimensional checks on machined features like bores, depths, and tight-tolerance mating surfaces because they physically contact the part and are less thrown off by surface finish or reflectivity. If your workflow revolves around prismatic parts with a handful of critical dimensions, a touch probe will usually give you the most repeatable numbers without fussing over lighting or part color.
Optical and laser methods earn their place when you need speed across many points or can't risk touching the surface. Laser scanners rapidly capture dense point clouds on complex freeform shapes, castings, or soft materials, making them ideal for reverse engineering and full-surface comparison to CAD. Optical systems—whether structured light or camera-based—excel on small features, edges, and thin materials where a stylus might deflect or simply be too large to reach. The trade-off is sensitivity to surface finish, transparency, and ambient light, so they demand a more controlled setup.
A practical way to decide is to map out what you measure most often. If most parts have flat datum surfaces, holes, and pockets, touch probing keeps programming simple and the results easy to defend. If your workflow includes organic shapes, high point counts, or non-contact requirements, adding a laser or optical sensor will likely cut inspection time even if it takes more effort to validate. Many shops settle on a hybrid approach—touch probe for the critical few dimensions, laser or optical for the rest—rather than forcing one sensor to do everything.
What service intervals and calibration costs actually look like after year one
Once the first-year honeymoon ends, maintenance schedules shift from optional to unavoidable. Depending on the equipment, you might be looking at a calibration every six months or, on the more forgiving end, an annual check that resets tolerances and flags drift before it becomes a repair bill. The problem is that "recommended" rarely means "included." Most warranties cover defects, not the routine alignment or sensor recalibration that keeps readings trustworthy, so those line items appear on your invoice even if nothing has broken.
Costs vary widely, but expect calibration to run anywhere from a few hundred to over a thousand dollars per visit if specialized tools or certified technicians are required. Some providers bundle calibration with a full service interval, which can soften the sting, while others treat it as a separate dispatch fee plus labor. After year one, components like seals, filters, and reference standards often need replacement long before the core unit does, and skipping them to save money usually leads to a pricier corrective calibration later.
Real-world schedules also depend on usage intensity and environment. A unit running 24/7 in a dusty or high-vibration setting might need quarterly checks, while the same model in a clean, climate-controlled space can stretch to 12 or 18 months. Instead of relying on the manual's optimistic timeline, ask your service provider for a condition-based plan that uses usage logs or drift history to set the next interval. That approach tends to keep costs predictable and avoids paying for calibrations you don't yet need.
When a cheaper VMM brand ends up costing more in rejected parts
The sticker price on a low-cost VMM looks great until the measurement drift starts showing up mid-shift. One batch passes, the next fails the same dimensions, and suddenly the inspection room is arguing about whether the machine or the part is the problem. Operators learn to distrust the readings, so every borderline feature gets rechecked two or three times, and still the data doesn't line up with the CMM results from the lab.
That mismatch is exactly where rejected parts begin to multiply. A machine that can't hold its edge detection or stage repeatability will reject good parts as out of tolerance and pass bad ones as acceptable. The rejects might be scrapped or sent through costly rework, while the false passes end up at the customer's incoming inspection and come back as complaints. Either way, the cost per part climbs quietly, often hidden in scrap reports and overtime rather than on the purchase order.
Then there's the downtime. Cheaper VMM brands frequently lack local service support, so a dead controller or a failed stage bearing can leave the machine parked for weeks. Every hour it's down, the line either runs blind or stops entirely. Add up the scrap, the rework, the extra inspection labor, and the delivery penalties, and the "savings" from that budget machine disappear several times over. A more reliable VMM with solid repeatability and fast support would have paid for itself before the first quarterly review.
FAQ
Focus on the machine's accuracy specifications, build quality, and the software that comes with it. A brand with a solid track record in your industry is often a safer bet than one that just offers a lower price.
There are several well-regarded names like Mitutoyo, Nikon, and OGP, but your choice depends on the specific part sizes and tolerances you work with. Smaller brands can also deliver excellent value if their local support is strong.
The software is often the deciding factor. Even the most accurate machine will frustrate you if the measurement routines are clunky or hard to automate. Ask for a demo with your own parts before committing.
Sometimes yes, if your tolerances are not extremely tight and you don't need advanced features like multisensor integration. However, for sub-micron work, the proven brands tend to hold calibration longer and come with better error mapping.
This is critical. A brand with local technicians and quick response times will save you days of downtime. Check how long they've been in your region and whether they offer on-site training during installation.
That depends on your production volume. For high-mix, low-volume work, a manual machine might be fine. But if you're measuring hundreds of parts a day, look for a brand that offers robust CNC automation and batch programming.
A specialized brand often has more refined edge detection and lighting options, which matter for complex geometries. General suppliers can be convenient for multi-instrument purchases, but their VMM software may feel like an afterthought.
Conclusion
Spec-sheet accuracy figures rarely survive first contact with real parts. Surface finish, edge irregularities, and lighting changes can easily push a machine outside its stated tolerance, so trusting a brand name without testing it on your own components is a gamble. The three manufacturers that dominate precision inspection each have genuine strengths, but they also fall short in predictable ways: one struggles with fixturing flexibility, another buries useful features in convoluted software, and a third demands premium pricing for support that may not arrive quickly. Before you commit, run a short capability study with your most challenging part geometries, not just the vendor's polished demo block.
Choosing between optical, laser, and touch probe is less about which is "best" and more about what your inspection workflow actually tolerates. Reflective surfaces often need laser, deep bores may require touch, and optical is fast but sensitive to edge contrast. After year one, service intervals and calibration costs can quietly double your operating budget, especially if the machine sits in a harsh environment. A cheaper VMM brand might look attractive on paper, but when false passes let bad parts through or false failures choke production, rejected parts and rework quickly erase the initial savings. Match the machine to your parts, test before buying, and price in lifecycle costs rather than the sticker.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/